Laser marking: contrast is a surface condition, and it changes with the alloy
Two marks specified as the same grey can differ by a factor in legibility, because annealed marking depends on the oxide and engraved marking depends on the depth.
Two mechanisms, one machine
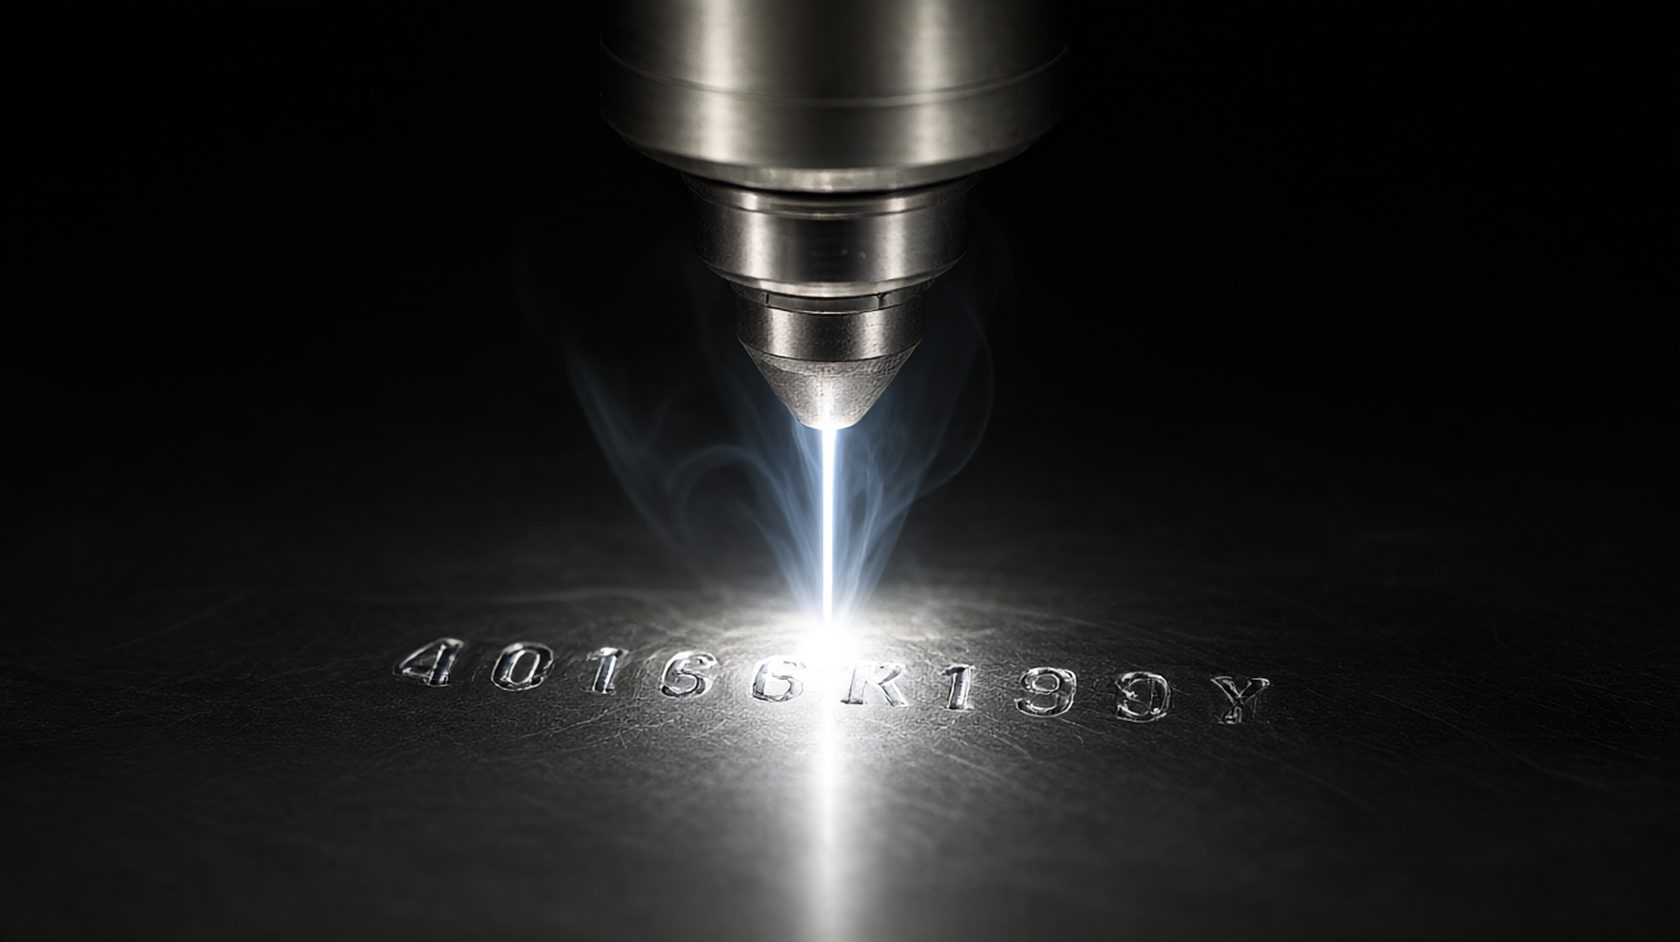
A fibre laser marks metal by annealing the surface, by melting it, or by ablating it. Annealing produces a colour change with no material removal; melting produces a shallow recast; ablation removes material and leaves a depth.
The three mechanisms produce three different marks, and the same machine can produce all three by changing the power density and the pulse duration. A marking specification that names only a size has not named a mechanism.
Annealing is the most legible on stainless and the least durable on a surface that is later passivated, because the passivation removes the oxide that carries the colour. A mark that is annealed and then pickled disappears.
Ablation is the most durable and the least attractive, because it leaves a depth that collects dirt. A mark on a food-contact surface that is ablated is a mark that will be described as unhygienic.
Contrast on stainless: the oxide and the angle
Annealed contrast on stainless comes from a thin oxide film whose thickness sets the interference colour, and the film grows with heat input. A low heat input gives a pale yellow, a higher one a dark grey, and too much gives a rough black that is actually melted.
The contrast is also a function of the surface finish: a brushed surface scatters and reads grey, a polished surface reflects and reads dark. The same mark on two finishes measures differently and looks differently.
The viewing angle matters because the oxide is iridescent. A mark that reads strongly at normal incidence can be nearly invisible at a grazing angle, and a customer who tilts the part sees nothing.
The specification should name the mechanism, the target contrast measured on the production finish, and the viewing geometry. A contrast figure without a finish and an angle is a figure that cannot be reproduced.
Depth, recast and the fatigue that starts at a mark
An engraved mark is a notch, and a notch on a cyclically loaded part is a crack initiation site. A serial number on a rotating shaft is the reason shafts fail at the number rather than at the fillet.
The recast layer around an engraved mark is harder and more brittle than the base, and it is also a corrosion site. A mark on a part that is later passivated has a recast layer that the acid attacks differently from the base.
The depth should be specified as a maximum as well as a minimum, because a legible mark is not a deep mark. A 20 micron mark is legible on most alloys and a 100 micron mark is a groove.
The specification should state the depth range, whether recast is acceptable, and whether the mark is in a stressed region. A mark placed without a stress check is a mark that shortens the part's life.
Marking on a coated or a plated surface
A mark on a zinc-plated or a painted surface removes the coating locally and exposes the steel. That is acceptable when the mark is cosmetic and unacceptable when the coating is the corrosion protection.
A mark through a powder coat leaves a ring of disbonded coating around the mark, which is the starting point for a blister. The ring is visible under a microscope and it grows in a salt spray.
The alternative is a mark applied before coating, or a mark applied through a mask that is removed before coating. Both are process sequences rather than marking parameters.
The specification should name the coating, the marking sequence relative to coating, and the touch-up if any. A mark on a coated part without a sequence is a mark that is sometimes applied before and sometimes after.
Speed and the mark that is a line of dots
A fibre laser mark is built from overlapping spots, and the overlap sets the edge quality. At high speed the spots do not overlap and the mark is a line of dots that reads as a dotted edge; at low speed they overlap and the mark is solid.
The overlap is set by the spot size, the frequency and the speed, and the three are linked. A specification that names speed without frequency and spot size is a specification of one third of the condition.
The dotted edge is visible at magnification and it is also a functional problem on a small character, because a 1 mm character built from dots is not a character. Small text needs a tighter overlap than large text.
The specification should state the character height, the stroke width and the overlap, and should include a magnified first-off check. A mark that is legible at arm's length and dotted at ten times is a mark that fails a supplier audit.
The fixture that keeps the focus
A marking head has a shallow depth of focus, and a part that is not flat moves in and out of focus across the mark. A mark that is sharp at one end and blurred at the other is a focus problem.
The depth of focus for a typical 160 mm lens is a few millimetres, and a part with a 5 mm step needs either a taller lens or a repositioning between marks. A taller lens increases the spot size and reduces the power density.
The fixture has to hold the part at a known height and orientation, and a part that is located on a rough surface varies by the surface's roughness. A cast surface located on the as-cast face varies by several millimetres.
The specification should state the focus height with a tolerance and the datum the fixture locates on. A fixture that locates on a rough face is a fixture that makes the focus random.
Readability: the standard the mark has to meet
A mark carrying a part number or a date code has to be readable by a person and by a machine, and the two requirements differ. A person reads contrast; a scanner reads edge definition.
The relevant standard for a barcode or a data matrix sets a grade from A to F, based on contrast, modulation, defects and quiet zone. A mark that looks good to a person can grade D because of a low edge contrast.
The grade should be verified with a verifier at the production mark, not with a phone application. A phone application reports a decode, not a grade, and a decode at grade D is a mark that a warehouse scanner will fail.
The specification should state the symbology, the grade and the verification method, and should include the grade in the first-off record. A mark specified without a grade is a mark specified by appearance.
Dust, fume and the lens that slowly loses power
Marking and engraving produce fume and dust, and the dust deposits on the protective lens. A lens with a deposit absorbs power and the mark fades over a shift, which reads as a drifting parameter.
The extraction has to be at the mark, not at the cabinet, because the plume rises from the mark and disperses. An extraction at the cabinet removes the fume after it has passed the lens.
The lens should be cleaned on a count of marks rather than on a schedule, and the cleaning should be recorded. A lens cleaned with the wrong solvent is a lens with a coating damage that no cleaning fixes.
The specification should state the extraction position, the lens cleaning interval and the power check. A power check with a meter at the start of each shift converts a drifting mark into a measured one.
The mark that has to survive a lifetime
A nameplate mark on an industrial part has to survive cleaning, painting and handling, and the durability is a test rather than an assumption. A mark that is rubbed with a solvent and a cloth is a mark that either stays or does not.
The test is an abrasion and a solvent rub to a stated standard, with the mark assessed for legibility after each. A mark that passes the rub and fails the solvent is an annealed mark on a part that will be cleaned.
The durability also depends on the mechanism: ablation survives almost everything, annealing survives almost nothing chemical. A part that is cleaned with an alkaline detergent needs an ablated or a deep annealed mark.
The specification should state the cleaning the part will see and the durability test that represents it. A mark specified for a part with no cleaning requirement is a mark specified for a different product.
A laser marking specification in eight lines
Eight lines cover a laser mark: mechanism (annealed, melted or ablated), character height and stroke width, overlap with spot size and frequency, depth range with recast acceptability, contrast measured on the production finish at a stated angle, focus height with the fixture datum, symbology grade with the verification method, and a durability test that represents the part's cleaning.
The lines convert a mark from an appearance into a process, which is what a supplier audit asks for. A mark specified by a picture is a mark that cannot be rejected.
The two lines that decide legibility in the field are the contrast measured on the real finish and the symbology grade, because both are usually checked on a polished coupon instead of a production part.
Write the eight, keep a marked first-off from each setup, and re-qualify when the finish, the coating or the lens changes. A new lens is a new spot size.
A marking system specified with a contrast figure measured on the production finish is the fiber laser marking machine, and the finish is what a coupon test cannot reproduce.
- 01Mechanism named: annealed, melted or ablated, not simply “laser marked”.
- 02Character height and stroke width stated, with the overlap that makes a solid edge.
- 03Depth range with a maximum, and a statement on recast acceptability.
- 04Contrast measured on the production finish at a stated viewing angle.
- 05Focus height with a tolerance, and the fixture datum named.
- 06Symbology grade A to F with a verifier, not a phone decode.
- 07Durability by abrasion and solvent rub, matched to the part's cleaning.
- 08Extraction at the mark, lens cleaning on a mark count, power checked each shift.